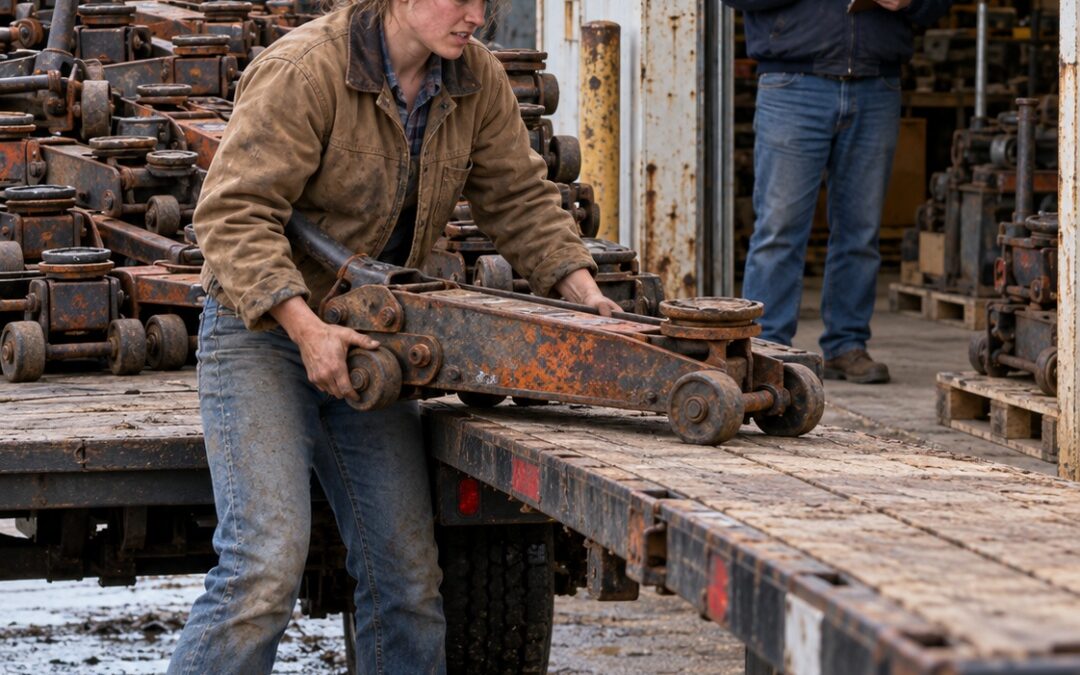
The district manager watched me load his 700 rusted floor jacks and called them “paper weights.” I was 26, borrowing a flatbed, and I didn’t argue with a man who’d spent years around hydraulic equipment. I only made him sign the receipt for every one—because in the notebook beside me, I’d already underlined one number twice: $4.
The engine ticked as I pulled into our lane, and Dad heard the borrowed truck before he saw what was sitting behind it.
Otis came out of the machine shed and waited while I drove past the cedars.
He was in his early sixties then, over six feet tall but beginning to stoop through the shoulders after forty years over machinery. His hair had gone white beneath the gray seed cap. In one hand was the steel click-type torque wrench he’d carried for decades.
Dad looked at the load.
Then he walked its entire length.
Slowly.
He stopped beside one jack, turned the release, and watched the saddle fall without resistance.
“They give these away?”
“They paid to be rid of them.”
That part made sense to him.
The rest didn’t.
We went inside for dinner.
Afterward, I put my notebook on the kitchen table.
Now I finally explained the $4.
A comparable new floor jack cost around $200.
What I suspected was that a large share of Fairholt’s jacks had failed because their cup seals had dried, hardened and cracked after sitting.
The seal kit cost about four dollars.
If I was right about even half of them, the arithmetic was ridiculous.
Dad didn’t laugh.
He found the weaknesses.
Oil.
Storage.
Time.
The corner of his shed I wanted was the same corner he needed when the combine head came in for winter work.
And underneath all those practical objections was the one that mattered.
If my theory was wrong, I wasn’t wrong once.
I was wrong seven hundred times.
Dad folded his reading glass.
“I need to think about it.”
That was not permission.
But it wasn’t no.
Two mornings later, I entered the machine shed before daylight was fully up.
Dad was already there.
He turned from the bench holding an old glass canning jar filled with clean amber hydraulic oil.
He held it toward me.
“Corner’s yours till the head goes back in the combine in March.”
There were conditions.
Keep the oil off his floor.
Keep the rust contained.
Don’t ask him to help lift any of them.
Then came the warning.
“If you’re wrong about the seals, you’re wrong about seven hundred of them.”
I took the jar.
That was Dad’s version of trust.
The next weekends became hauling weekends.
Four trips.
Seven hundred floor jacks.
Roy was there for several of them, still clicking his pen and calling them paper weights.
On the last trip, he joked that he almost ought to charge me for the diesel just so the deal felt fair.
I thanked him for the receipt.
Then I drove away.
By mid-October, seven hundred jacks occupied a chest-high wall of iron in Dad’s shed.
The smell was rust and old oil.
Standing in front of them was different from seeing them on a loading dock.
Seven hundred is a very large number when it’s inside your own building.
Dad’s warning returned immediately.
Wrong seven hundred times.
So I stopped looking at the wall.
I started looking at one jack.
Then another.
Pump.
Load.
Watch the saddle.
Check the ram.
Record the result.
Thirty seconds.
Next jack.
My notebook developed its own language.
Pumped and held.
Pumped and drifted.
Wouldn’t pump.
Cracked casting.
Bad ram.
Parts.
After about sixty jacks, patterns began appearing.
But I wouldn’t let myself count them yet.
I needed evidence.
So I chose one of the most promising jacks and put it on the bench.
Sockets.
Old screwdrivers.
Snap-ring pliers.
Rags.
Then I opened it.
A hydraulic jack isn’t mysterious once it’s apart.
The handle moves a small pump piston.
The piston pushes oil through a check valve into the cylinder beneath a larger ram.
Oil doesn’t compress, so each stroke forces the ram upward.
Open the release and the oil returns.
Simple.
And almost everything expensive inside that first jack was fine.
The cast base was sound.
The polished steel ram cleaned up beautifully.
Pump piston—good.
Check valves—good.
Machined surfaces—good.
Then I reached the cup seals.
There it was.
The rubber had hardened.
The lip had cracked.
Instead of sealing against the bore and pushing oil, it let oil slip around it.
The entire heavy machine had been condemned because a small piece of rubber had gone hard.
Four dollars.
I bought the replacement kit.
Flushed the old oil.
Cleaned the bore.
Oiled the new seals.
Reassembled everything in reverse order.
Then I filled the reservoir with Dad’s clean amber oil.
The first pump stroke felt like mush.
So did the second.
My fingers tightened around the handle.
Third stroke.
Pressure.
Fourth.
Solid.
The polished ram began to rise.
I still didn’t trust it.
Dad had a loaded steel toolbox on the bench. I slid the jack underneath one end and pumped.
The saddle met the steel.
Then the toolbox lifted.
An inch.
Two.
I leaned my own weight against it.
The saddle stayed exactly where I’d put it.
No drift.
No settling.
One jack.
Behind me were 699 more.
That night, another question replaced the first.
One jack could lift one point.
What could hundreds of them do together?
Before I could answer that, I had to rebuild them.
I drove into Council Bluffs to a hydraulic and bearing supplier.
Verl Tuttle had been behind that parts counter for twenty-two years.
I gave him the seal-kit number.
Then I asked how many he had.
He checked.
I told him I wanted all of them and another couple hundred as soon as he could order them.
He looked at me.
Then he laughed.
Again, not cruelly.
Nobody ordered two hundred identical cup-seal kits.
“Two hundred?”
“Seven hundred eventually.”
The laugh stopped.
I explained what I’d found.
Fairholt jacks.
Cup seals hardened from sitting.
Sound castings.
Sound rams.
Four-dollar seal inside a roughly two-hundred-dollar jack.
Verl’s face changed before he said anything.
Technical language does that.
You can argue with a claim.
It’s harder to argue with somebody who has already had the machine apart.
He had around thirty kits available.
I bought them.
Then I ordered more.
That was the moment the experiment began costing actual money.
So I built a workflow.
Tear down.
Flush.
Inspect.
Rebuild.
Test.
Tag.
Repeat.
Ten became thirty.
Thirty became fifty.
By December, more than a hundred rebuilt jacks stood along the wall.
Fewer than one in ten were genuinely beyond saving.
Even those weren’t useless.
A cracked casting could still contain a good ram.
A ruined ram could sit above good check valves.
One dead jack could donate parts to several others.
Nothing left the shed without being questioned first.
Dad started a ledger.
He never announced it.
One morning it was simply sitting on the bench.
Date.
Jacks finished.
Seals bought.
Oil used.
And a running calculation of what buying equivalent new jacks would have cost.
Dad never told me the ledger meant he believed in the project.
He didn’t have to.
The numbers were doing it for him.
And those numbers pushed me toward the next idea.
A hundred individual jacks were useful.
A farm didn’t need a hundred individual lifts.
It needed a few enormous ones.
A grain wagon.
The rear of a tractor.
A loaded trailer.
No single salvaged floor jack could safely handle those jobs.
But hydraulic pressure doesn’t care how many cylinders receive it.
So I drew a system at the kitchen table.
One pump.
One reservoir.
A manifold.
Multiple hydraulic lines.
Several rebuilt jacks acting together.
One machine with many hands.
The first rig used eight jacks under an oak beam beneath the rear of a loaded hay wagon.
Word had spread by then.
Four or five men appeared along the fence the morning I tested it.
Dell Harmon from the implement dealership was there.
Dad stood closer to the shed with his torque wrench.
Nobody knew whether the thing would work.
Including me.
I closed the release valve.
Started pumping.
The hoses stiffened as pressure built.
Eight saddles touched the beam.
The loaded wagon began rising.
One inch.
Then two.
Conversation at the fence stopped.
It worked.
For about another second.
A hydraulic union let go with a crack like a rifle.
Amber oil sprayed.
The loose hose whipped against the beam.
The load shifted.
Then the wagon dropped.
Hard.
I’d placed timber blocking beneath it.
The wagon slammed onto those blocks.
They held.
Nobody was hurt.
That was the good part.
Oil dripped from the beam.
The men at the fence didn’t laugh.
That somehow made it worse.
One by one, they found reasons to leave.
Dell Harmon was last.
Dad walked down after everyone else had gone.
He inspected the blocking.
The broken union.
The hose.
Then he said only one thing.
I’d blocked it right.
After dark, I sat alone on an overturned bucket.
For the first time since the Fairholt dock, quitting became a serious option.
I had a hundred working jacks.
I could sell them slowly.
Recover my money.
Stop building rigs.
Let the county forget the wagon hitting those blocks.
It was sensible.
So I gave the idea the same treatment I’d given the jacks.
I took it apart.
What had actually failed?
Not the lifting.
The eight jacks had lifted the wagon.
The problem was sharing the load.
Their strokes weren’t perfectly identical.
Some reached the end of their travel first.
When one stopped contributing, the remaining cylinders inherited more load.
Pressure concentrated.
The weakest fitting failed.
That wasn’t a law of nature.
It was a design problem.
And design problems can be changed.
I measured the stroke of every rebuilt jack.
Then I matched sets whose travel stayed within roughly a sixteenth of an inch.
But mechanical matching wasn’t enough.
Loads move.
Beams aren’t perfectly flat.
One saddle can contact first.
Pressure still needed somewhere to go.
So I redesigned the manifold.
Instead of treating each jack as an isolated branch from the pump, I bored a common gallery connecting all eight ports.
Oil could move sideways.
If one jack began taking too much load, pressure increased at that port.
Oil moved through the gallery toward lower-pressure cylinders.
The system could rebalance itself.
I oversized the unions.
Sealed every thread.
Used Dad’s torque wrench.
Then I brought the loaded hay wagon back.
No spectators this time.
Just Dad.
Eight matched jacks.
Oak beam.
Balancing manifold.
And blocks.
Always blocks.
I pumped.
The saddles rose together.
Then the wagon moved.
Flat.
One inch.
Two.
Four.
Six.
Eight.
All eight rams climbed as one.
I stopped pumping.
Waited.
Nothing drifted.
I pushed against the wagon.
The manifold redistributed the change.
Still level.
The whole rig cost roughly $110 in materials.
A commercial portable hydraulic wagon lift of comparable usefulness was around $2,900.
That number didn’t need underlining.
Dad came out the next morning.
The wagon had remained elevated overnight exactly where I’d left it.
He walked around the rig.
Sighted down the rams.
Pressed his weight against the wagon frame.
Then he looked at the manifold.
“That’s a good manifold.”
He paused.
“I wouldn’t have thought to let the oil move sideways like that.”
Dad went back inside.
I stayed beside the rig.
That was enough.
Soon the first truck came up our lane.
A farmer named Sherwood brought me a dead three-ton jack he’d been ready to dump.
Black oil.
Grit.
Hard, split cup seal.
Same disease.
I rebuilt it for the cost of the seal and oil.
It went back under his combine and held.
Then another farmer came.
Then another.
Dead jacks began appearing beside the shed door.
I didn’t advertise.
Farmers did it for me.
Save somebody two hundred dollars and he’ll usually tell somebody else.
The multi-jack rig grew too.
Eight jacks became twelve.
It lifted tractors.
Loaded hay trailers.
Equipment that normally required expensive commercial lifting systems.
The principle remained the same.
Matched cylinders.
Common pressure.
Balanced load.
Dad’s ledger kept growing.
By the end of the second year, it showed more than $40,000 worth of new jacks people hadn’t needed to buy.
I still charged neighbors only for seals and oil.
Then the story traveled back to Roy Kesler.
Three years after he watched me load the first truck, somebody mentioned my operation while buying equipment from him.
Roy learned that the floor jacks he’d given away were working again.
More than that, they had become the basis of an entire lifting system.
His pen stopped clicking.
I didn’t know any of this until a Saturday when a car—not a farm truck—came slowly up our lane.
I stepped to the shed doorway wiping my hands on a rag.
Roy got out.
Same stocky build.
Same navy jacket.
Gray slacks this time.
Black shoes that looked completely wrong in a farmyard.
No clipboard in his hand.
He looked past me.
Rows of rebuilt jacks lined the wall.
Tagged.
Measured.
Tested.
The lifting rig stood nearby.
Roy walked inside.
Slowly.
He examined the jacks.
Then the manifold.
He crouched and looked at the gallery ports.
Nineteen years around hydraulic equipment meant he understood exactly what he was seeing.
He straightened.
His laugh lines weren’t moving now.
“I was wrong.”
Nothing after it.
No excuse.
No qualification.
Just three words.
I could have opened Dad’s ledger.
I could have shown him the savings.
I could have reminded him about the paper weights.
Instead I said:
“I know.”
Because I did.
But Roy hadn’t driven out there because he had to.
He could have stayed home forever.
Instead he’d driven to somebody’s farm on a Saturday to say three words that cost him something.
That mattered.
Then he did something more useful.
Fairholt was closing additional depots.
Two more locations had piles of returned and failed hydraulic equipment scheduled for disposal.
Floor jacks.
Bottle jacks.
Transmission jacks.
Other hydraulic units.
Roy signed those disposal orders.
He told me he’d route the equipment to me before it reached the crusher.
Free.
Same terms.
Only now he knew exactly what I would do with it.
He wrote the depot addresses down.
I folded the paper into my notebook.
Verl changed too.
He didn’t make a speech.
He simply started sending customers to me.
Men would come to his counter with a dead jack and see the price of a replacement.
Verl would tell them about the woman outside Oakland who might fix theirs for the cost of a seal.
That was his version of saying he’d learned something.
Then Dell Harmon returned.
He had been standing at the fence when my first lifting rig failed.
Now he came as an implement dealer.
He tested one of my rebuilt jacks himself.
Pumped it.
Felt it take pressure.
Then asked:
“What would you take for twelve?”
Until then, I’d mostly given away my labor.
Now I had to price the work.
I calculated the seal.
Oil.
Time.
What the jack was worth.
What Dell needed for margin.
Then I gave him a number.
He didn’t bargain.
He wrote the check.
I loaded twelve rebuilt floor jacks into his truck.
The same worn paint.
The same old castings.
But nobody called them scrap this time.
The first year selling through Dell, I rebuilt and sold about 190.
Then roughly 340.
Then more than 500.
Eventually I hired someone part-time for teardown while I kept working on pumps and manifolds.
Then the farm economy turned.
Dry years.
Low prices.
Debt.
Neighbors who had borrowed against land and machinery began losing operations they’d spent their lives building.
There was nothing satisfying about watching it.
Dad had survived hard agricultural years by refusing to borrow against ground he couldn’t afford to lose.
Without realizing it, I’d built my hydraulic operation on the same principle.
My raw material had been free.
A seal cost four dollars.
Oil was paid for.
The shed already existed.
There was no large loan underneath the business.
No expensive inventory financed against the farm.
Nothing for a bad year to pull on.
And during those lean years, rebuilt equipment became more attractive.
A farmer who couldn’t justify a $200 new jack could still justify an $80 rebuild.
So while stronger-looking operations struggled under debt, our shed light stayed on.
The work expanded.
Hydraulic cylinders.
Bottle jacks.
Loader components.
Rams.
Check valves.
Every discarded machine asked the same question.
What is actually bad?
By the turn of the century, more than a thousand rebuilt units were moving through the operation each year.
Two men handled teardown.
I still worked on the pumps.
A trade publication eventually wrote about the operation.
Then an equipment show in Kansas City asked me to speak.
I left the invitation sitting on the kitchen table for a week.
Standing behind a workbench made sense to me.
Standing behind a podium did not.
Dad was in his seventies by then.
More stooped.
Slower.
Same gray seed cap.
Same torque wrench.
He read the invitation through his little chest-pocket magnifier.
“Well,” he said, “you already know the answer.”
So I went.
Years later, another vehicle came up Bradock Lane.
A small red car.
A young woman stepped out carrying a laptop under one arm and a spiral notebook in the other.
Kayla.
My brother’s daughter.
She’d come home from school with a degree in metals and materials.
“Aunt Nella, I want to show you something.”
Then she did something familiar.
She asked to walk the shed first.
Kayla didn’t spend much time looking at the rebuilt jacks.
She went to the cull pile.
Cracked castings.
Scored bores.
The roughly ten percent I’d long ago classified as genuinely finished.
Scrap.
She opened her notebook.
Started sketching.
I walked over.
“What do you see?”
She showed me.
A cracked casting meant the casting was finished.
Not necessarily the ram.
Not the gland.
Not the check valves.
Not the pump.
The pile I’d stopped seeing as useful wasn’t garbage.
It was inventory.
Sound components were sitting inside bad shells.
Exactly the mistake Fairholt had made with the seven hundred jacks.
Only this time I was the one making it.
I looked at Kayla’s numbers.
Fifteen years earlier, I’d put numbers in front of Dad and waited two days for permission.
I wasn’t going to make her wait.
“Bench is open,” I told her. “Take whatever you need off the pile.”
Kayla spent the next week dismantling it.
The scrap heap became labeled bins of usable components.
Then I gave her the sentence Dad had given me.
Never throw a part away before you’ve questioned it every way you know how.
Kayla wrote it down.
Dad was sitting nearby with the old torque wrench across his knees.
He heard his words leave my mouth and enter her notebook.
He didn’t say anything.
He stayed in the chair a little longer.
The operation is still there on Bradock Lane.
I’m older now.
Gray at the temples beneath a faded green cap.
Kayla runs the parts side.
Together, the operation eventually moved more than 1,600 rebuilt units a year across nine counties in two states.
The ledger’s second column passed $2 million over the decades.
And the thing that started it was still absurdly small.
A new floor jack cost around $200.
The seal that could stop it from working cost about $4.
The difference was never the weight of the iron.
It was whether somebody had stopped asking questions.
Out in the yard, the lifting rig is still doing the job I first imagined in that notebook.
A row of rebuilt cylinders.
Oil moving through the common gallery.
Pressure sharing itself from one jack to another.
A loaded wagon rising level.
Then stopping.
Steady.
The rams hold it there.
And the shed light stays on.