I gave a hauler $180 to leave nine “frozen” lathes at a closed Missouri trade school instead of taking them to the scrapyard. He laughed at the bargain, and the parts-store owner later told me I should buy a new machine. I had only one dial reading to trust. Then a gunsmith bent over the barrel I’d just cut and stopped moving.
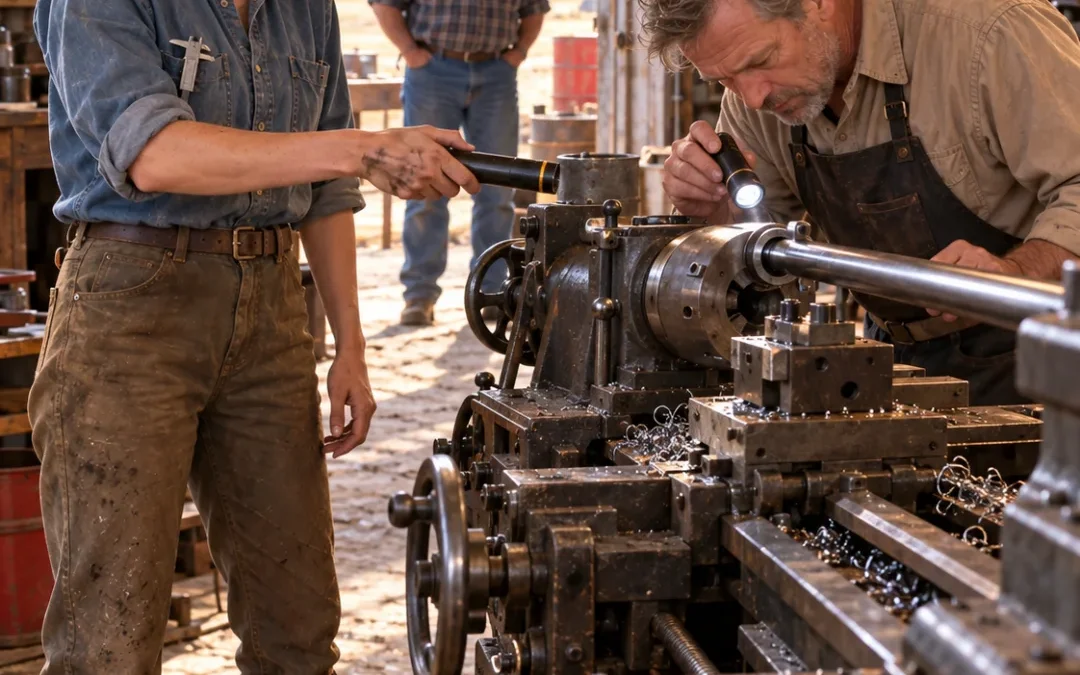
Roy held the bore light against the barrel and looked down the chamber.
I stood beside the lathe with the machine stopped. A few minutes earlier, its heavy bed had taken the cutting force without passing chatter into the barrel. The reamer had gone in slowly, cutting cleanly through the steel. Now all that was left was what the light showed him.
Roy looked for a long time. Then he raised his head, looked at me, and bent over the barrel again.
The chamber walls were smooth and bright. No rings. No chatter marks.
He straightened up.
“What do I owe you?” he asked.
I thought about the work and the price I could stand behind. “Eighty-five dollars.”
He counted the money into my hand beside the fender. I asked if he wanted a receipt.
“I surely do,” he said.
I wrote one on a page from my notebook and tore it off. He folded it into his shirt pocket, picked up the barrel, and held it carefully. Before he climbed into his truck, he said he’d be back within the month with two more. He knew four other gunsmiths who had been fighting chatter on their own machines. He would tell them about the shop outside Shell City.
Then he drove away.
The dust settled back onto the gravel. I had $85 in my shirt pocket, next to the caliper. In the notebook was the receipt stub. One man had brought a job, watched me do it, and paid for it. He knew four others.
That was enough to go back to work.
I covered the lathe and picked up my scraper. Five more beds still needed to be brought true.
The machines had cost me $180 for the hauling, plus the materials I’d bought to rebuild them. I had not purchased a ready-made business. I had bought old iron for the price of taking it away, and I had spent two winters learning what it could do.
The word reached Court Havson in pieces.
Court had run his parts counter for 19 years. When I’d gone in to buy scraping stock, abrasive, and blue, he had told me I should buy a new machine. New lathes ran faster, came with warranties, and were ready to use. He had not meant to dismiss me. He had believed the facts he knew led to the safest answer.
The first story he heard was that I had chambered a barrel for Roy. Then another customer said it. Then a third person repeated it. Court did not come out the first time he heard. He kept serving customers and weighing what he knew against what people were saying.
In October, nearly a year after I’d bought the supplies from him, he drove up the Kesler lane on a Saturday. I heard his truck before I saw him. The grainery door stood open, and I had a barrel in the chuck.
I didn’t turn around. The reamer was in the cut, and I wasn’t going to walk away from it. I fed it in, brought it to depth, cleaned the chips, gauged the chamber, and backed it out. Only after the spindle stopped did I lay the barrel on the bench and wipe my hands.
Court stepped inside. He looked at the lathe and at the chamber. Then he said, “I was wrong.”
He said it plainly, without making excuses. I did not ask him to say more.
“It’s the beds,” I told him. “Cast iron that’s had 80 years to settle. It doesn’t move anymore.”
Court told me his store had a back room of tooling that had come in through trades and closeouts: collets, chucks, reamers, and attachments for machines that were no longer made. He had been selling it for scrap. He offered to let me look through it at the scrap prices.
He also said he’d been sending people with hard jobs to Kansas City. He would start directing them to Shell City.
That was not charity. It was the thing he knew how to do: point the traffic toward work he trusted.
At supper, I told my father Court had come by, admitted his mistake, and offered tooling and referrals. Warren listened over his plate.
“Turned out you looked at it closer than the rest of them,” he said.
It wasn’t an apology. He had read my figures, taken two days to think, and let me try. Now the proof was in the work.
“Even if it had never cut a chamber, it was paid for,” I said.
My father looked at me across the table. “A thing that’s paid for can’t be taken back.”
I had grown up hearing that line about land, machinery, and the difference between a note and a deed. Now I understood it in a new way. The lathes were mine. No bank held a claim on one casting.
The customers came gradually. First from Missouri, then from Kansas and farther away. Men drove up the Shell City road with barrel blanks in padded boxes because my machine could hold a cut that their own equipment could not. They came because someone they trusted had tried the work.
I kept writing everything down. I charged what the work cost: machine time, my time, tooling, and a fair wage for skill. A chamber job stayed $85 even when more trucks arrived. I could have charged more. I didn’t.
In the part year of 1993, I completed a little over 60 jobs and took in more than $5,000. In 1994, the book showed about 240 jobs and just over $19,000. By 1995, the total had passed $30,000.
The nine lathes each got a dedicated job. One was set for chambering. Another handled muzzle crowns. Others took threading, barrel contours, shaft work, and repairs. Once I had a setup right, I left it there. A shop with one lathe spends hours changing it over. My row of machines could keep working without losing the same time to setup after setup.
I brought them online one by one. In the fall of 1995, I hired Junior Petri, a 19-year-old from Vernon County who came asking to learn. I started him on cleanup and the simplest machine jobs. I watched him work for a month before I brought him near the chambering lathe.
“I’ll show you everything,” I told him. “The day you can hold a tenth without me watching, I’ll pay you like a man who can hold a tenth.”
He learned carefully. By the next year, he was running three of the dedicated machines. I kept the scraping work for myself.
Junior, my father, and I added onto the grainery. We poured a proper slab and moved the heavier lathes onto it. The shop grew by earning what it needed. I paid for each board and each bag of concrete before I laid it.
By then, the order book ran three or four weeks ahead.
In 1998, the hog market collapsed, and corn prices followed. Men who had borrowed to build confinement barns or buy machinery found themselves owing on equipment worth far less than the loan. Auction bills went up around the co-op. Some of those men had stood nearby years earlier while people joked about the “boat anchors” up the Shell City road.
My father went to one sale to stand with a neighbor. He came home quiet.
The downturn did not touch my shop in the same way. I owed nothing on the lathes. The work came from gunsmiths who needed barrels chambered whether hogs sold for a dollar or a dime. The grainery kept humming, with Junior at his machines and me at the chambering lathe.
“Over supper, the paid-for things are the ones still standing,” Warren said one evening.
I had no answer to add.
In the summer of 2006, Alan Rydorf drove up in a rental car too clean for the Shell City gravel. He wrote for a machine-trade monthly and had heard about my shop from people who had used it. I let him in because he had asked plainly.
He walked the row of nine machines. He thought at first that their old castings must have some lost quality, perhaps extra care or pride in the men who made them.
“It isn’t pride,” I told him. “Pride doesn’t hold a tenth. Mass does.”
I showed him the lathe bed and explained what the weight did. A cut pushed back against the machine; if the bed flexed, even slightly, that movement went straight into the part as error. These old castings had been poured heavy, then left through decades of freeze and thaw. The strain had worked out of the iron over time.
The article ran that fall. Rydorf asked to see my books, and I showed him. Letters arrived from machinists in Pennsylvania and Oregon, and one from Scotland. An association in Kansas City invited me to speak to 300 men. I thanked them on the back of a feed-store receipt and declined. If someone wanted to understand how the work was done, I thought they should come watch.
By then I was 58. My hands had begun to slow. Junior was good, but I had never thought much about what might come after me. I was too busy keeping the work moving.
Then, on a cold, clear Saturday in the spring of 2011, my niece Dela drove up with a laptop bag and a spiral notebook. She was 22, fresh out of school, and carried her mother’s chin and my father’s level way of standing.
She opened the laptop on the bench. She had taught herself to search auction listings, estate sales, and shop closures for old tool-room lathes being sold by scrap weight. She had already found 11 machines in four states. She wanted to bring them to Shell City, rebuild them, and learn scraping from me.
I sat with the caliper in my pocket and listened to her plan. I remembered the kitchen table, my father’s careful figures, and the two days I’d waited for his answer.
Dela had come ready to argue her case.
I didn’t make her wait.
“Yes,” I said. “When can you start?”
That afternoon, I showed her which lathe carried the chambering setup, why it stayed set, and how to feel a bearing coming true under a scraper. Toward evening, we stood over a stripped bed with a straightedge and a can of blue.
I gave her the line my father had given me.
“What you’ve squared the money on stays yours for good.”
Dela wrote it in her notebook.
The iron on the bench had been paid for. The work had been measured and tested. And beside me stood someone who wanted to learn how to see what the rest of the world had priced by the pound.